Tá Luoyang Anjing Intelligence Equipment ina cheannaire domhanda i bhfoirnéisí leictreacha ardteochta
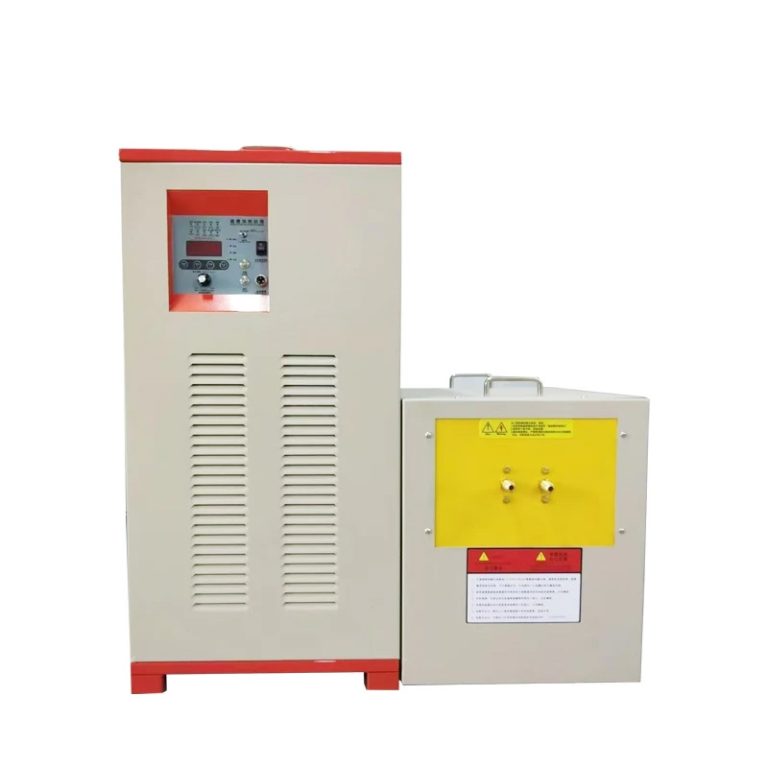
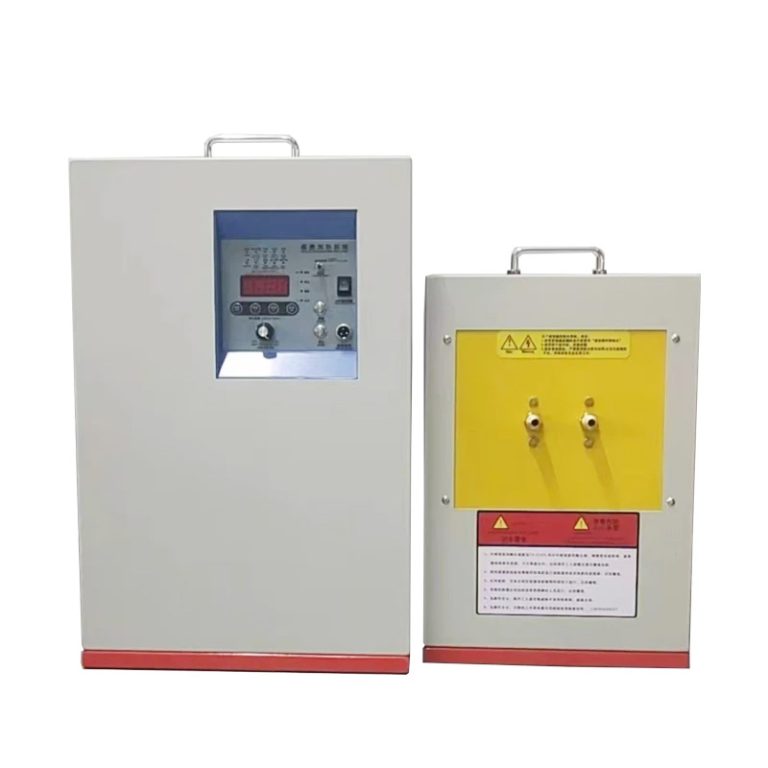
Foirnéise Téimh Ábhar Soladach Meán-Minicíocht


Paraiméadair TÁIRGÍ
Cur síos
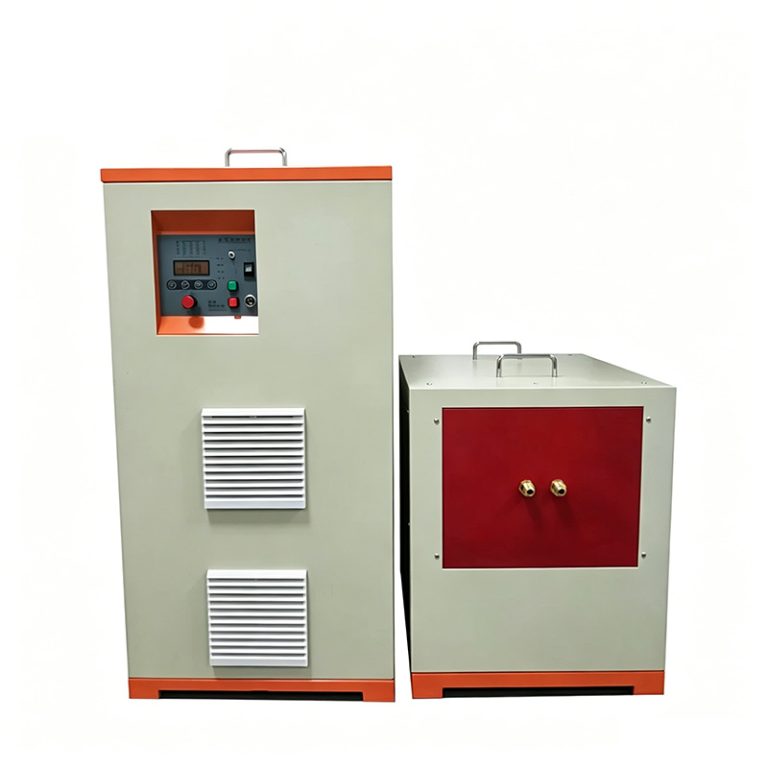
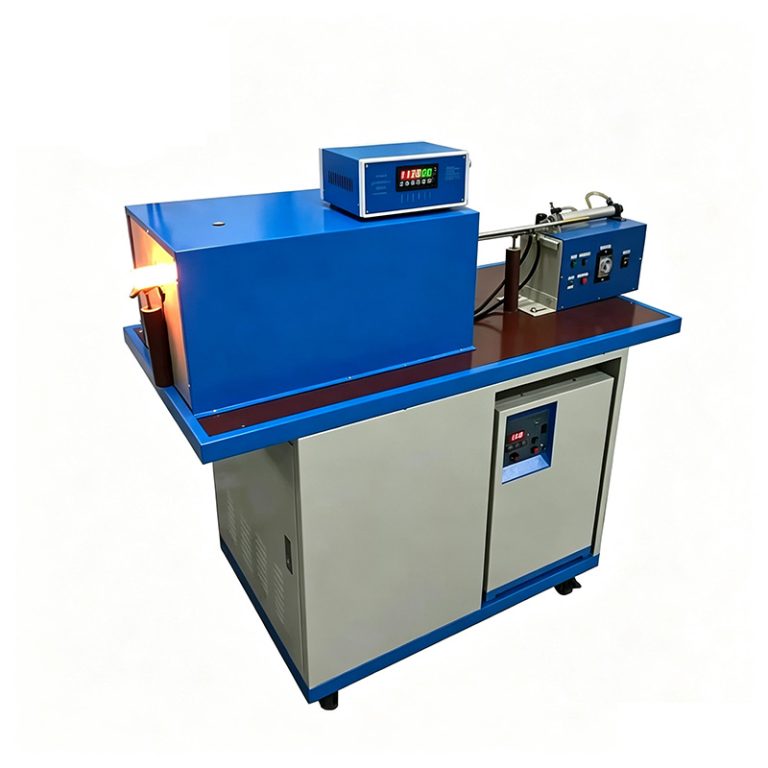
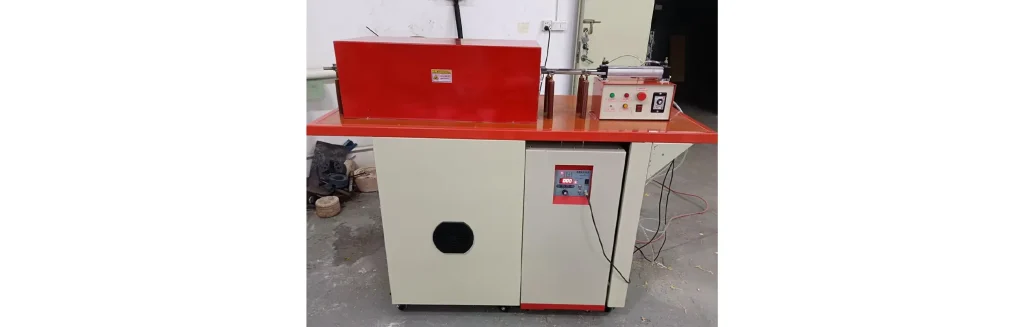
Medium-frequency induction heating furnace
A medium-frequency induction heating furnace is a device that uses medium-frequency induction heating technology to rapidly heat metal bars, billets, and irregularly shaped billets. It is widely used in forging, upsetting, extrusion, and hot forming processes. The equipment is particularly suitable for continuous through-heating of steel (≥Φ12mm), cruach dhosmálta, copar, alúmanam, and other non-ferrous metals.
Through the principle of medium-frequency electromagnetic induction, heat is generated directly inside the workpiece, achieving rapid heating and deep heat penetration. The equipment can perform overall workpiece heating or, depending on process requirements, localized heating methods such as end heating or center heating, providing a stable and efficient heat source for modern forging production.
Gnéithe Táirge
- Designed for Continuous Through-Heating of Metal Bars
This equipment is a medium-frequency forging furnace, specifically designed for the continuous through-heating of round bars, square billets, and irregularly shaped billets made of steel (≥Φ12mm), cruach dhosmálta, copar, alúmanam, and other metals.
- Wide Frequency Range for Precise Matching of Bar Size
With a frequency range of 1-20kHz, the optimal frequency can be selected based on the bar diameter and material type to achieve optimal penetration depth and heating uniformity.
- High-Efficiency Through-Heating Design
Induction coil lengths range from 500mm to 1 meter, allowing simultaneous heating of multiple bars to ensure completely uniform material temperature.
- Continuous and Stable Heating with Minimal Power Fluctuations
The continuous feeding structure keeps the induction load stable, avoiding drastic fluctuations in power demand during single-bar heating (from room temperature to 1100℃).
- IGBT technology, 15-20% more energy efficient than thyristor systems
Utilizing an IGBT-based design, compared to traditional thyristor-based intermediate frequency power supplies, it can save 15-20% in energy consumption, occupy less space, and is easier to maintain. It boasts extremely high power factor and power supply efficiency across the entire power range, significantly reducing operating costs.
| Model | Heating to 1050℃ (Cruach Dhosmálta) | Heating to 700℃ |
|---|---|---|
| AJ-35F | 1.25 kg/min | 1.75 kg/min |
| AJ-45F | 1.67 kg/min | 2.33 kg/min |
| AJ-70F | 2.50 kg/min | 3.50 kg/min |
| AJ-90F | 3.33 kg/min | 4.67 kg/min |
| AJ-110F | 4.17 kg/min | 5.83 kg/min |
| AJ-160F | 5.83 kg/min | – |
| AJ-240F | 8.60 kg/min | – |
| AJ-300F | 11.25 kg/min | – |
| AJ-500F | 17.90 kg/min | – |
Réimsí Iarratais
- Hot Forging Preheating: Suitable for preheating steel, cruach dhosmálta, copar, alúmanam, and other metal bars and billets before hot forging.
- Bar End Upsetting and Forming: Suitable for localized heating and upsetting of bar ends.
- Continuous Heating of Round and Square Bars: Suitable for large-scale continuous heating of round and square bars.
- Local Hot Forming or Extrusion: Suitable for localized hot forming and hot extrusion processes of metal bars.
- Online Forging Production: Suitable for online forging heating processes of parts such as gears, slata nascadh, agus crankshafts. Seamlessly integrates with forging production lines to achieve continuous and automated production.
- Hot Rolling Preheating: Suitable for preheating metal bars and billets before hot rolling. Provides uniform heating, minimizes oxidation and burning loss, and improves rolling quality.
Próifíl na Cuideachta
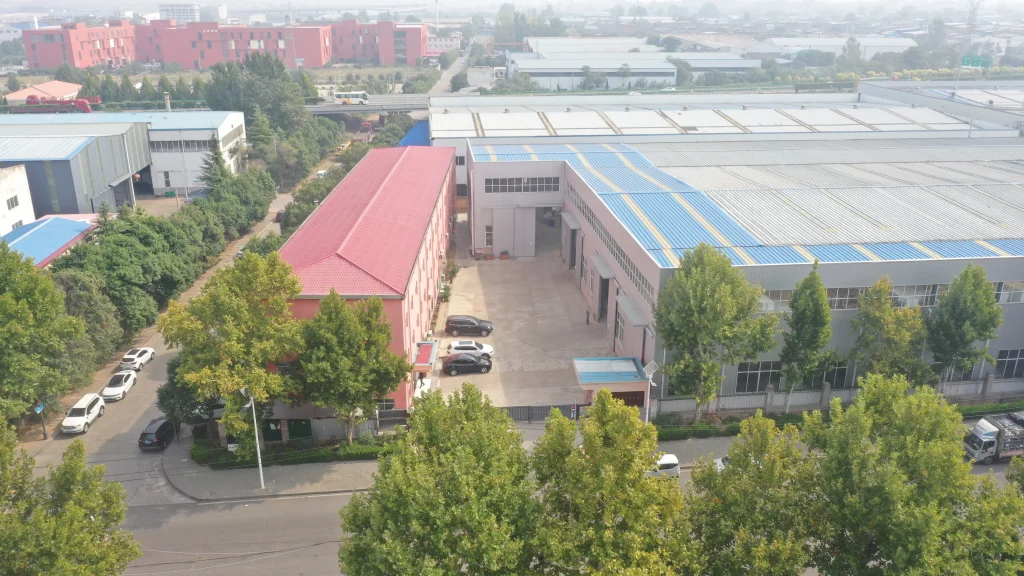
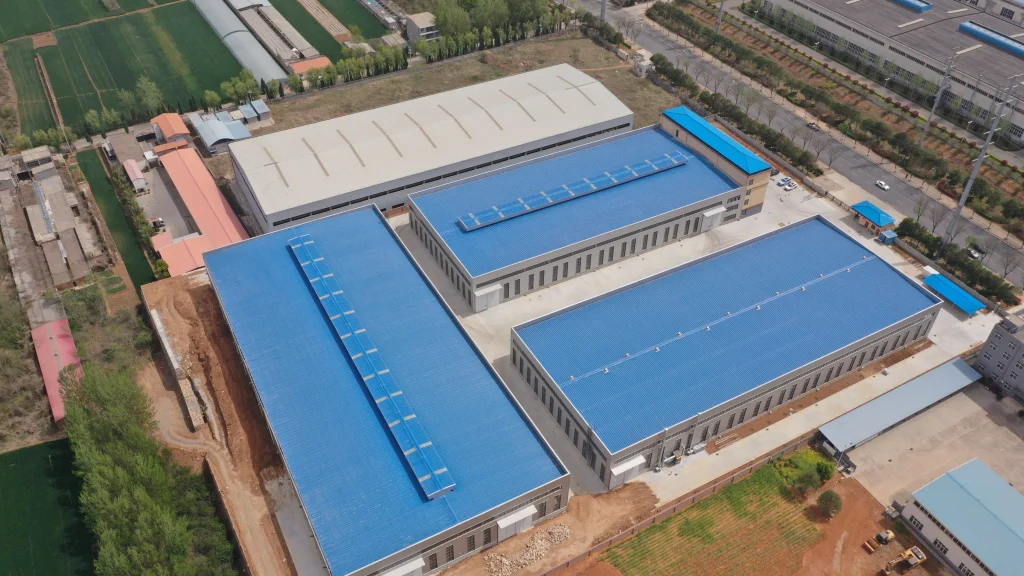
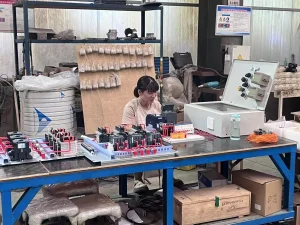
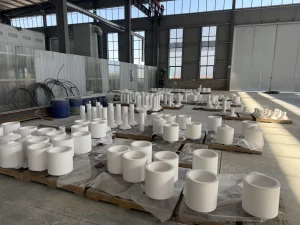
Is fiontar gairmiúil atá ag speisialú i seirbhísí teicneolaíochta cóireála teasa agus an R&D, déantúsaíocht, agus díolachán foirnéisí leictreacha ardteochta.
Díríonn an chuideachta ar fhoirnéisí leictreacha ardteochta a fhorbairt a chlúdaíonn raon teochta iomlán de -100 ℃ go 2600 ℃. Áirítear ar a chuid táirgí foirnéisí leictreacha turgnamhacha, foirnéisí atmaisféar bhfolús, áitheanna tionsclaíochta, agus trealamh téimh ionduchtaithe meánmhinicíochta. I measc na dtáirgí is mó tá foirnéisí bosca, foirnéisí feadán, foirnéisí ardaithe, áitheanna pusher, foirnéisí bogie, áitheanna rothlacha, áitheanna tolláin, agus foirnéisí meán-minicíochta speisialaithe éagsúla.
Cloíonn an chuideachta le nuálaíocht theicneolaíoch agus tá deimhnithe ISO9001 agus CE an AE faighte aici. Is leis 21 trádmharcanna cláraithe, 29 paitinní, agus 27 cóipchearta bogearraí.
Modhanna Íocaíochta
TT
Modhanna Loingsiú
Tá an foirnéis leictreach pacáistithe i dtrí shraith: fillte ar dtús i páipéar cúr, fillte ansin i scannán plaisteach, agus ar deireadh pacáilte i gcliathbhosca adhmaid.
Ceisteanna Coitianta (CCanna)
- What materials are suitable for the medium-frequency forging heating furnace?
Suitable for heating and preheating of carbon steel, cruach cóimhiotail, cruach dhosmálta, copar, alúmanam, and other non-ferrous metals.
- Can the equipment achieve localized heating?
Tá. The equipment supports overall through-heating, as well as end heating, center heating, and localized heating of designated areas.
- What size bars are suitable for heating?
Generally suitable for round bars, square bars, and irregularly shaped billets with a diameter of Φ12mm or more. Specific specifications can be customized according to customer needs.
- Can the equipment be used in automated production lines?
Tá. The equipment adopts a continuous feeding design and can be matched with automatic feeding, conveying, and forging equipment to achieve automated production.
- How energy-efficient is the equipment?
Utilizing IGBT medium-frequency inverter technology, it typically saves 15%-20% energy compared to traditional thyristor medium-frequency equipment, effectively reducing production costs.